How to Store Hydraulic Cylinders and Prevent Corrosion
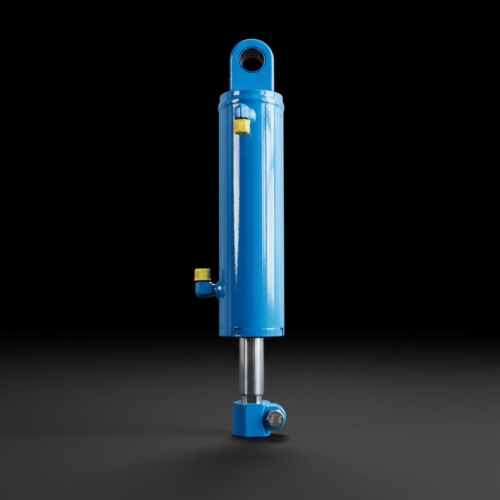
Store hydraulic cylinders clean, dry, capped, identified, and protected from corrosion, contamination, impact, and unsupported handling loads.
Руководства по осмотру, уплотнению и техническому обслуживанию гидравлических цилиндров.
Store hydraulic cylinders clean, dry, capped, identified, and protected from corrosion, contamination, impact, and unsupported handling loads.
Remove a stuck hydraulic cylinder pin by fully supporting the load, unloading the joint, identifying retainers, and applying controlled extraction force.
A welded hydraulic cylinder is normally serviced through its removable gland or retainer while the welded base remains part of the barrel assembly. Identify the retention method, support the tube without crushing it and inspect the welded structure before replacing seals.
Rebuilding a telescopic hydraulic cylinder requires documenting stage order, stop components, seals, wear rings and port paths before disassembly. Each stage must be measured and inspected separately because one damaged tube or incorrect seal can disrupt sequencing and load support.
Polish a hydraulic cylinder rod only to remove very light raised contamination or staining within an approved surface-finish process. Polishing cannot replace missing chrome, correct deep scoring or restore an undersized rod. Measure defects and coating condition before removing material.
Manual extension or retraction is possible only when displaced oil has a controlled path and the load is mechanically secured. Identify cylinder type, valve state and trapped-pressure devices before applying external force. Never push against sealed ports or an unsupported load.
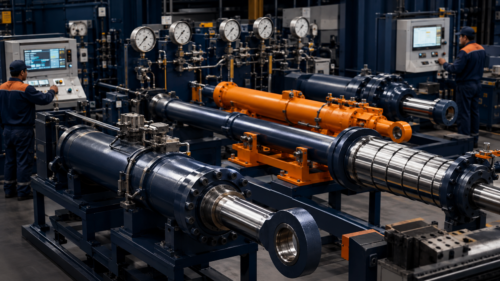
Hydraulic cylinder lubrication normally comes from the operating fluid. During assembly, apply only a clean, compatible assembly lubricant to seals, bearings and sliding surfaces. External grease belongs only on specified pins, spherical bearings or mounting interfaces, not on the exposed rod as a universal remedy.
Install a hydraulic cylinder seal kit only after confirming every seal profile, size, material and orientation against the cylinder record. Cleanliness, protected edges and controlled assembly are essential because a new seal can be damaged before the cylinder is pressurized.
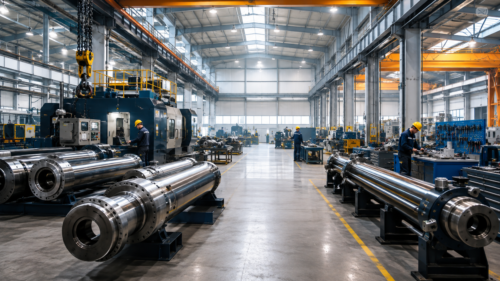
Honing a hydraulic cylinder bore is a controlled machining and finishing process used to correct minor surface damage and establish the specified geometry and crosshatch. It is not a way to hide deep scoring, excessive taper, out-of-round condition or a barrel that would exceed dimensional limits.
Hydraulic cylinders are normally filled through a clean hydraulic circuit rather than poured full as isolated components. Use the specified compatible fluid, connect both ports correctly, maintain reservoir level and cycle slowly so oil displaces air without cavitation or uncontrolled movement.
 English English
 Russian
 Spanish
 Arabic
 French
 Portuguese
 Vietnamese